


Packaging of pharmaceuticals plays a vital role in the modern pharmaceutical industry. The transportation and distribution process of pharmaceuticals needs to ensure that the quality, safety and efficacy of pharmaceuticals are safeguarded to meet the needs of patients and the requirements of healthcare organizations. In this process, aluminum foil pharmaceutical packaging plays an important role in providing comprehensive protection and stability for medicines, the following are some aspects of its importance:
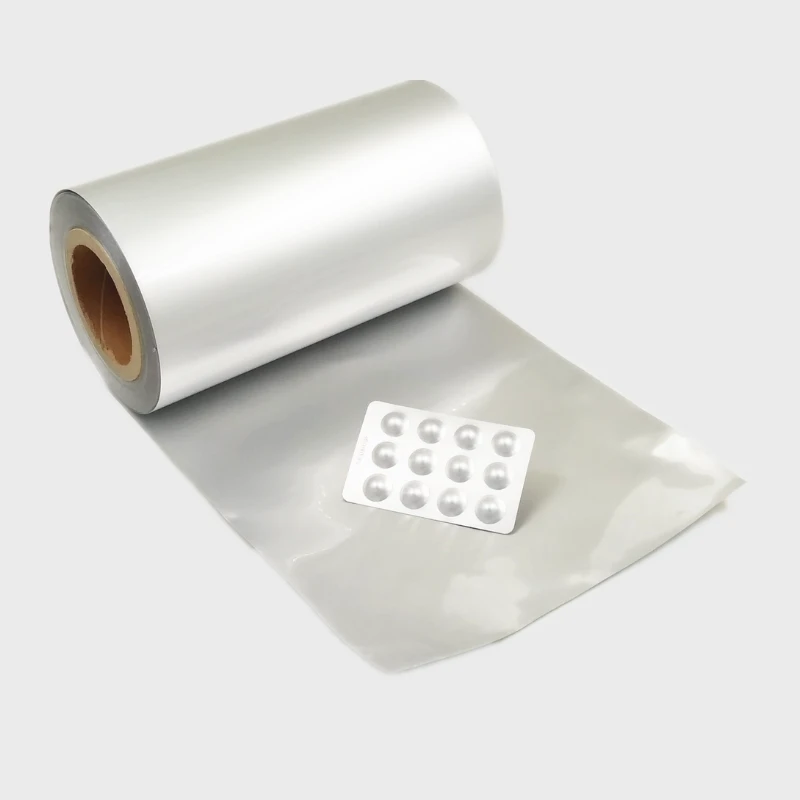
1. Protective Properties: Medicines may be affected by light, moisture, oxygen and other environmental factors which may deteriorate and reduce the effectiveness of the medicines. Aluminum foil pharmaceutical packaging can provide an effective barrier to prevent these harmful factors from entering the pharmaceutical container, thus maintaining the stability and long-term effectiveness of the drug.
2. Anti-counterfeiting safeguard: Medicines are susceptible to the risk of counterfeiting and forgery during transportation. Aluminum foil packaging has unique materials and characteristics that make counterfeiting more difficult. Manufacturers can use specific logos, patterns and anti-counterfeiting technologies on aluminum foil packaging to ensure the authenticity of medicines and protect patients from counterfeit medicines.
3. Package sealing: Aluminum foil packaging can effectively guarantee the sealing of medicines, preventing them from leaking or being contaminated during transportation and distribution. This is essential to maintain the purity and potency of the medicine.
4. Storage stability: Aluminum foil packaging reduces the exposure of medicines to the external environment, thus maintaining the stability of medicines during storage. The chemical properties of medicines may change under the influence of factors such as light, temperature and humidity, and aluminum foil packaging can provide an extra layer of protection to reduce these effects.
5. Doctor-patient trust: The quality and safety of the packaging of medicines has a direct impact on the trust in the doctor-patient relationship. The use of reliable packaging materials, especially aluminum foil pharmaceutical packaging, helps to improve patient confidence in the quality and efficacy of medicines and enhances the reputation of the healthcare system.
6. Increased availability of medicines: Aluminum foil pharmaceutical packaging extends the shelf life of medicines, thus allowing them to be distributed and used in more remote locations. This is particularly important for patients in remote areas, who also have access to high quality pharmaceutical treatments.
7. Environmental Advantage: Aluminum foil pharmaceutical packaging is often recyclable, helping to reduce the amount of waste generated by the packaging. This is in line with society's concern for sustainability and environmental protection, and helps the pharmaceutical industry play an active role in sustainable development.
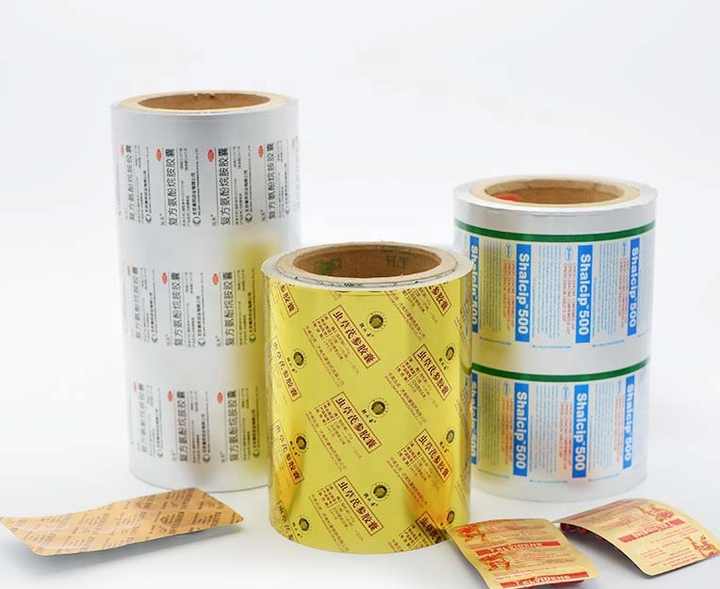
Protecting the physical integrity of medicines: Medicines are susceptible to crushing, vibration or impact during transportation, which can lead to physical breakage. Aluminum foil pharmaceutical packaging has a certain degree of pressure resistance and shock resistance, which can effectively protect the physical integrity of medicines and reduce the risk of damage to medicines.
Extending the shelf life of medicines: Some medicines are prone to degradation after exposure to the external environment, resulting in weakening of their efficacy. Aluminum foil pharmaceutical packaging ensures that patients receive high-quality medication by insulating them from the external environment and slowing down the rate of degradation, thereby extending the shelf life of the medication.
Provides security: Aluminum foil pharmaceutical packaging often has special security features, such as engravings, patterns, or color variations, that can help identify genuine medicines, reduce the risk of counterfeiting, and ensure patient safety.
Meet regulatory and quality requirements: The pharmaceutical industry is subject to strict regulations and quality requirements, and the packaging materials for pharmaceuticals also need to comply with the relevant regulations and standards. Aluminum foil pharmaceutical packaging, as a commonly used compliance packaging material, meets these regulations and requirements, ensuring that pharmaceuticals are in compliance during transportation and distribution.
Aluminum foil pharmaceutical packaging plays an important role in the transportation and distribution of pharmaceuticals. It protects medicines from harmful factors, maintains their stability and effectiveness, extends their shelf life and provides anti-counterfeiting features, thus ensuring that patients receive safe and effective medication. Against the backdrop of the ongoing development of the pharmaceutical industry, aluminum foil pharmaceutical packaging will continue to play a key role in providing patients with better drug protection.