


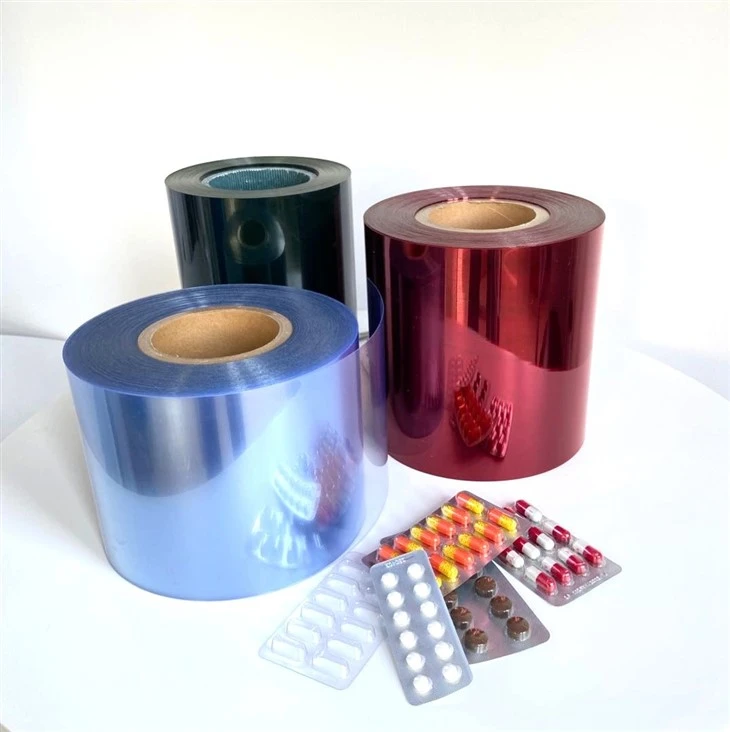
Products Description
Crystal-Clear PVC/PVDC Laminates: High-Gloss Finish & Maximum Product Visibility with Zero Compromise on Barrier
In today's competitive B2B landscape-where shelf appeal directly drives purchase decisions and product integrity is non-negotiable-ordinary packaging laminates force brands to make a costly tradeoff: either prioritize visibility to attract customers or focus on barrier protection to preserve product quality. Our Crystal-Clear PVC/PVDC Laminates shatter this compromise entirely, delivering a perfect synergy of premium aesthetics and uncompromising protection. Engineered for brands that refuse to settle for "good enough," these laminates combine ultra-transparent clarity, a sleek high-gloss finish, and industry-leading moisture/oxygen barrier performance-all in a single, easy-to-process material that elevates your product's presence while safeguarding its integrity from production to end-use.
Unlike generic clear films that become hazy, yellow, or brittle over time, or barrier films that hide your product behind opaque layers, our PVC/PVDC laminates are crafted with precision to maintain their crystal-clear appearance and barrier performance for the entire product lifecycle. Whether you're packaging pharmaceutical tablets, premium confectionery, high-end nutraceuticals, or consumer health products, these laminates turn your packaging into a marketing tool-showcasing your product's quality while ensuring it stays fresh, potent, and compliant with global standards.

Key Product Features: Where Clarity Meets Uncompromising Barrier
Ultra-Clear, Distortion-Free Optics: Crafted with high-purity PVC substrates and a precision PVDC coating, our laminates offer 92%+ light transmittance and near-zero haze-providing unobstructed visibility of your product's color, texture, and details. No more cloudy or foggy packaging; your tablets, capsules, or confections will stand out with a "glass-like" clarity that immediately signals premium quality to retailers and end-users.
Premium High-Gloss Surface: The smooth, high-gloss finish enhances printed graphics, brand logos, and product details with exceptional vibrancy and sharpness. Unlike matte or semi-gloss films, our laminates reflect light evenly, creating a luxurious, professional appearance that elevates shelf presence and helps your product stand out among competitors.
Advanced PVDC Barrier Layer (No Compromise): The integrated PVDC layer delivers industry-leading moisture and oxygen blocking-without sacrificing clarity. Our laminates achieve an oxygen transmission rate (OTR) as low as 0.2 ml/m²·24h (ASTM D3985) and a water vapor transmission rate (WVTR) of 0.15 g/m²·24h (ASTM F1249), effectively preventing oxidation, hydrolysis, deliquescence, and discoloration of sensitive products.
Strong Interlayer Bonding: Engineered with a proprietary lamination process, our PVC/PVDC layers bond tightly together-eliminating delamination risks during thermoforming, heat-sealing, high-speed packaging, or long-distance shipping. This ensures consistent performance and reduces production waste caused by layer separation.
Clarity-Retaining Thermoformability: Unlike standard clear films that cloud or distort when formed, our laminates maintain their crystal-clear appearance even after deep drawing (up to 15mm forming depth). This makes them ideal for blister packaging, where crisp, transparent cavities showcase your product while providing secure protection.
Consistent Heat-Seal Performance: Designed for seamless integration with high-speed blister and packaging lines, our laminates form airtight, leak-proof seals at a wide range of temperatures (120–160℃). The strong seal integrity prevents moisture, oxygen, and contaminants from entering, preserving product freshness and extending shelf life.
Dimensional Stability & Processability: Uniform thickness (18–45μm) and stable web tension ensure smooth feeding and minimal wrinkling or web breakage on high-speed lines (up to 300 packs per minute). This reduces downtime, improves production efficiency, and lowers overall operational costs.
Pharma & Food-Safe Formulation: Manufactured under strict cleanroom conditions (Class 100,000) with pharmaceutical-grade raw materials-free from harmful plasticizers (e.g., DEHP), heavy metals, residual monomers, and volatile organic compounds (VOCs). Fully compliant with global food-contact (FDA 21 CFR, EU 10/2011) and pharmaceutical (USP Class VI, EP) standards.
UV & Aging Resistance: The PVDC layer also provides UV protection, preventing product discoloration caused by light exposure. Additionally, our laminates resist yellowing, brittleness, and optical degradation even after 24+ months of storage in varied environmental conditions (humidity 30–80%, temperature -20℃ to 60℃).

Rigorous Quality Control & Testing: Guaranteed Performance
We understand that B2B partners rely on consistent, reliable packaging materials-and we back our laminates with strict quality control and third-party testing. Every batch undergoes comprehensive inspection to ensure it meets our high standards:
Optical Performance Testing: Automated and manual checks for light transmittance, haze, clarity, and surface defects (e.g., scratches, bubbles, streaks). Only laminates with near-perfect optics pass our quality control.
Barrier Property Testing: Precise measurement of OTR (ASTM D3985, GB/T 19789) and WVTR (ASTM F1249, GB/T 1037) to ensure barrier performance meets your exact requirements. Test reports are available for every batch.
Laminate Adhesion Test: Pull-testing to verify interlayer bonding strength (≥5 N/15mm), ensuring no delamination during processing or shipping.
Thermoforming Clarity Test: Post-forming inspection to confirm clarity is retained after deep drawing, with no clouding or distortion.
Seal Strength & Integrity Testing: Pressure and leak tests to validate airtight seals, ensuring no moisture or oxygen ingress.
Safety & Purity Analysis: Testing for heavy metals (Pb, Cd, Hg <1 ppm), residual monomers (VCM <1 ppm), plasticizer migration, and microbial load (bacteria <100 CFU/g, mold <30 CFU/g) to meet pharma and food-safety standards.
Accelerated Aging & Environmental Testing: Simulated storage conditions (temperature cycling, high humidity, UV exposure) to confirm long-term stability and optical performance.
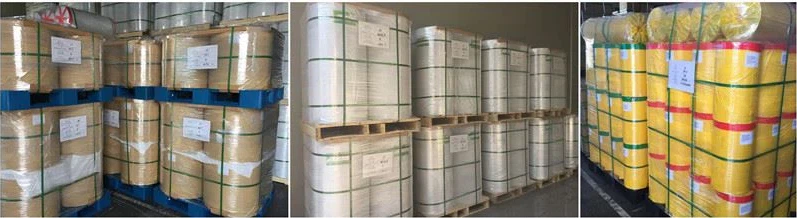
Core Functions & Business Benefits: More Than Just Packaging
Our Crystal-Clear PVC/PVDC Laminates don't just protect your product-they drive value for your business by solving real-world B2B challenges:
Boost Shelf Appeal & Brand Perception: The crystal-clear clarity and high-gloss finish turn your packaging into a silent salesperson, highlighting your product's quality and differentiating it from competitors. Retailers prioritize products with eye-catching packaging, and our laminates help you secure prime shelf space.
Preserve Product Integrity & Extend Shelf Life: The superior PVDC barrier prevents moisture and oxygen ingress, protecting sensitive ingredients (e.g., APIs, probiotics, vitamins) from degradation. This extends shelf life by 2–3x compared to standard clear films, reducing spoilage, product recalls, and waste.
Reduce Production Costs & Waste: Consistent thickness, dimensional stability, and strong interlayer bonding minimize production defects (e.g., delamination, wrinkling, poor seals). This lowers scrap rates, reduces downtime, and improves overall production efficiency.
Simplify Global Compliance: Fully compliant with major international standards, our laminates eliminate the need for separate packaging solutions for different markets. We provide complete documentation (CoA, test reports, compliance certificates) to support your regulatory filings and audits.
Enhance Printability & Traceability: The smooth high-gloss surface improves ink adhesion, allowing for high-quality flexographic or gravure printing, foiling, and serialization. This supports brand consistency, product traceability, and anti-counterfeiting efforts.
Adapt to Diverse Product Needs: Suitable for a wide range of sensitive products, from small tablets to large capsules, and compatible with various packaging formats (blister packs, sachets, pouches). Our laminates can be customized to meet your specific barrier, thickness, and width requirements.

Why Partner With Us for Your Crystal-Clear Laminates?
As a leading manufacturer of custom packaging films, we don't just supply materials-we partner with you to solve your unique challenges. Here's what sets us apart from competitors:
Specialized Expertise in Clear Barrier Laminates: With 18+ years of experience, we focus exclusively on high-clarity, high-barrier films-ensuring our products are engineered to meet the specific needs of B2B clients in pharma, food, and consumer goods.
Customization Capabilities: We offer full customization of thickness (18–45μm), width (up to 2000mm), PVDC coating weight (40–120g/m²), and surface finish (high-gloss, semi-gloss) to match your exact product and production requirements.
Flexible Supply & Competitive Pricing: We support flexible MOQs (minimum order quantities)-from small trial batches (500kg) to large bulk orders-with competitive pricing and fast lead times (7–15 days for standard orders, 15–25 days for custom orders).
Free Samples & Technical Support: We provide free samples (up to 10 meters per configuration) for on-site testing, along with technical guidance to optimize your packaging line, adjust machine settings, and ensure seamless integration.
Global Compliance & Transparency: We supply complete documentation, including CoA, test reports, and compliance certificates, to support your regulatory efforts in markets worldwide (FDA, EU, China, etc.).
Reliable After-Sales Support: Our team of packaging experts is available 24/7 to troubleshoot production issues, address quality concerns, and provide ongoing support-ensuring your operations run smoothly.
Frequently Asked Questions (FAQ)
We've compiled the most common questions our B2B partners ask about our Crystal-Clear PVC/PVDC Laminates to help you make informed decisions quickly. If you have additional questions, our team is always available to assist.
Q: Will the high-gloss surface cause glare that hides my product? A: No. Our high-gloss finish is engineered to reflect light evenly, enhancing product visibility rather than causing glare. The smooth surface minimizes light distortion, ensuring your product's details are clearly visible from all angles-even under retail lighting.
Q: Can these laminates be used with cold-form blister machines? A: Yes. Our laminates are compatible with both thermoforming and cold-form blister machines. We can adjust the PVC/PVDC structure to meet the specific forming requirements of your equipment, ensuring consistent performance and clarity.
Q: How does the clarity compare to glass or PET films? A: Our laminates offer near-glass clarity (92%+ light transmittance) with the flexibility and processability of plastic. Unlike PET films, which can become brittle or yellow over time, our PVC/PVDC laminates maintain their clarity and flexibility for the entire product lifecycle.
Q: Can I add anti-fog properties to the laminate? A: Absolutely. We offer optional anti-fog coatings that prevent condensation from forming on the inside of the packaging-ensuring your product remains visible even in humid environments (e.g., refrigerated storage, tropical markets).
Hot Tags: crystal-clear pvc/pvdc laminates: high-gloss finish & maximum product visibility with zero compromise on barrier, China, manufacturers, suppliers, factory, customized, custom, wholesale, low price, free sample, blister packaging film supplier, release film supplier, oxygen barrier plastic film, non adhesive plastic film, laminated pe film, biodegradable plastic film


